

1. Pourquoi les acheteurs d’ateliers d’usinage trébuchent sur la « sélection de la vitesse de broche »
Lorsque les acheteurs évaluent des machines CNC Doosan, les trois pertes les plus courantes dans l’approvisionnement d’un atelier d’usinage proviennent toutes d’une inadéquation entre paramètres et pièce.Point de douleur 1 : vitesse achetée trop élevée, le couple ne tient pas. De nombreux ateliers courent après la vitesse et choisissent une broche à entraînement direct de 15 000 tr/min, pour découvrir un couple insuffisant à basse/moyenne vitesse lors de l’usinage en série d’acier 45# ou d’acier à roulements → ébrèchement de l’outil, mauvaise fragmentation des copeaux, rugosité de surface hors tolérance, ce qui force à réduire la vitesse et la profondeur de passe — le temps de cycle réel est alors inférieur de plus de 30 % à la capacité prévue.Point de douleur 2 : on ne compare que les spécifications de broche, en ignorant le plateau couple-vitesse. Les listes d’achat ne comparent que la colonne « vitesse max » sans vérifier la courbe de couple ni la puissance continue S1 à cette vitesse. Deux machines toutes deux annoncées à 8 000 tr/min — l’une à entraînement direct, l’autre par courroie — peuvent différer jusqu’à 40 % en couple à basse vitesse : la même opération passe sans problème sur l’une et déclenche une alarme « surcharge/calage » sur l’autre.Point de douleur 3 : on force les centres d’usinage à traiter de grandes pièces en caisson — rigidité et courses sont toutes deux insuffisantes. De nombreux ateliers usinent des carters de boîte de vitesses, des carters de réducteur et des bancs de machine sur de grands centres d’usinage verticaux. Le long porte-à-faux de broche et la grande distance entre la pointe de l’outil et les roulements de broche → vibrations, flexion de l’outil, dépassement de tolérance de position, et les paramètres de coupe sont réduits à l’extrême ; des pièces pesant des dizaines de tonnes poussent la charge de table près de sa limite, occupant des machines qui devraient usiner des moules et des pièces de précision. Ces pièces n’auraient jamais dû être assignées à un centre d’usinage vertical — elles relèvent d’une aléseuse horizontale.Ces trois points de douleur définissent la logique de sélection : déterminer d’abord la matière et le type de pièce → puis fixer la plage de vitesse → puis vérifier le couple et la puissance → enfin contrôler l’avance rapide pour verrouiller le temps de cycle.
Pain point 1: Speed bought too high, torque can't hold. Many shops chase high speed and choose a 15,000 rpm direct-drive spindle, only to find insufficient low/mid-speed torque when batch-machining 45# steel or bearing steel → tool chipping, poor chip breaking, surface roughness out of tolerance, forcing a reduction in speed and depth of cut — actual cycle time runs 30%+ below designed capacity.
Pain point 2: Only spindle specs are compared, the torque–speed plateau is ignored. Purchase lists compare only the "max speed" column without checking the torque curve and S1 continuous power at that speed. Two machines both rated 8,000 rpm — one direct-drive, one belt-driven — can differ by up to 40% in low-speed torque: the same operation runs smoothly on one and throws an "overload/stall" alarm on the other.
Pain point 3: Machining centers are forced to handle large box-type workpieces — rigidity and travel are both insufficient. Many shops machine gearbox housings, reducer casings, and machine beds on large vertical machining centers. The long spindle overhang and large distance from tool tip to spindle bearings → vibration, tool deflection, and position tolerance overshoot, and cutting parameters get throttled to a crawl; workpieces weighing tens of tons push the table load near its limit, occupying machines that should be cutting molds and precision parts. These workpieces should never have been assigned to a VMC in the first place — they belong on a horizontal boring machine.
These three pain points define the selection logic: determine material and workpiece type first → then set the speed range → then verify torque and power → finally check rapid traverse to lock in cycle time.
2. Doosan Model Comparison: Matching Benchmarks for Process/Material
The following are representative specs for common Doosan machine tools (DN Solutions); always verify against the latest technical brochure (options/versions vary).
| Model | Type | Max Spindle Speed | Spindle Motor | Low-Speed Torque Characteristic | Rapid Traverse X/Y/Z | Table Load | Best Fits |
|---|---|---|---|---|---|---|---|
| Lynx 2100 | Turning center | 4,500 rpm | 15 kW | High torque (strong mid/low speed) | 30 m/min | Disk/shaft class | Medium/large-diameter disk & shaft parts, carbon steel rough & finish turning |
| PUMA 2600 | Turning center | 3,500 rpm | 30 kW | Gearbox optional, heavy cutting | 30 m/min | Disk/shaft class | Large-diameter castings & forgings, heavy turning |
| DNM 4000/4500 | Vertical MC | 8,000 rpm (12,000–15,000 direct-drive option) | 18.5 kW | Direct-drive/high-torque option (4500 HT ≈ 286 N·m) | 36 m/min (48 option) | ≈ 600–800 kg | Steel, cast iron, aluminum (general) |
| DNM 5700 | Vertical MC | 8,000 rpm (15,000 option) | 18.5 kW | Spindle torque ≈ 118 N·m (HT option ≈ 286 N·m) | 36 m/min | ≈ 1,000 kg | Heavy die steel, medium-large box parts |
| DVF 5000 | 5-axis MC | 12,000 rpm (18,000 option) | 31 kW | High speed, high rigidity | 40 m/min | ≈ 500–800 kg | Complex aluminum surfaces, aerospace parts |
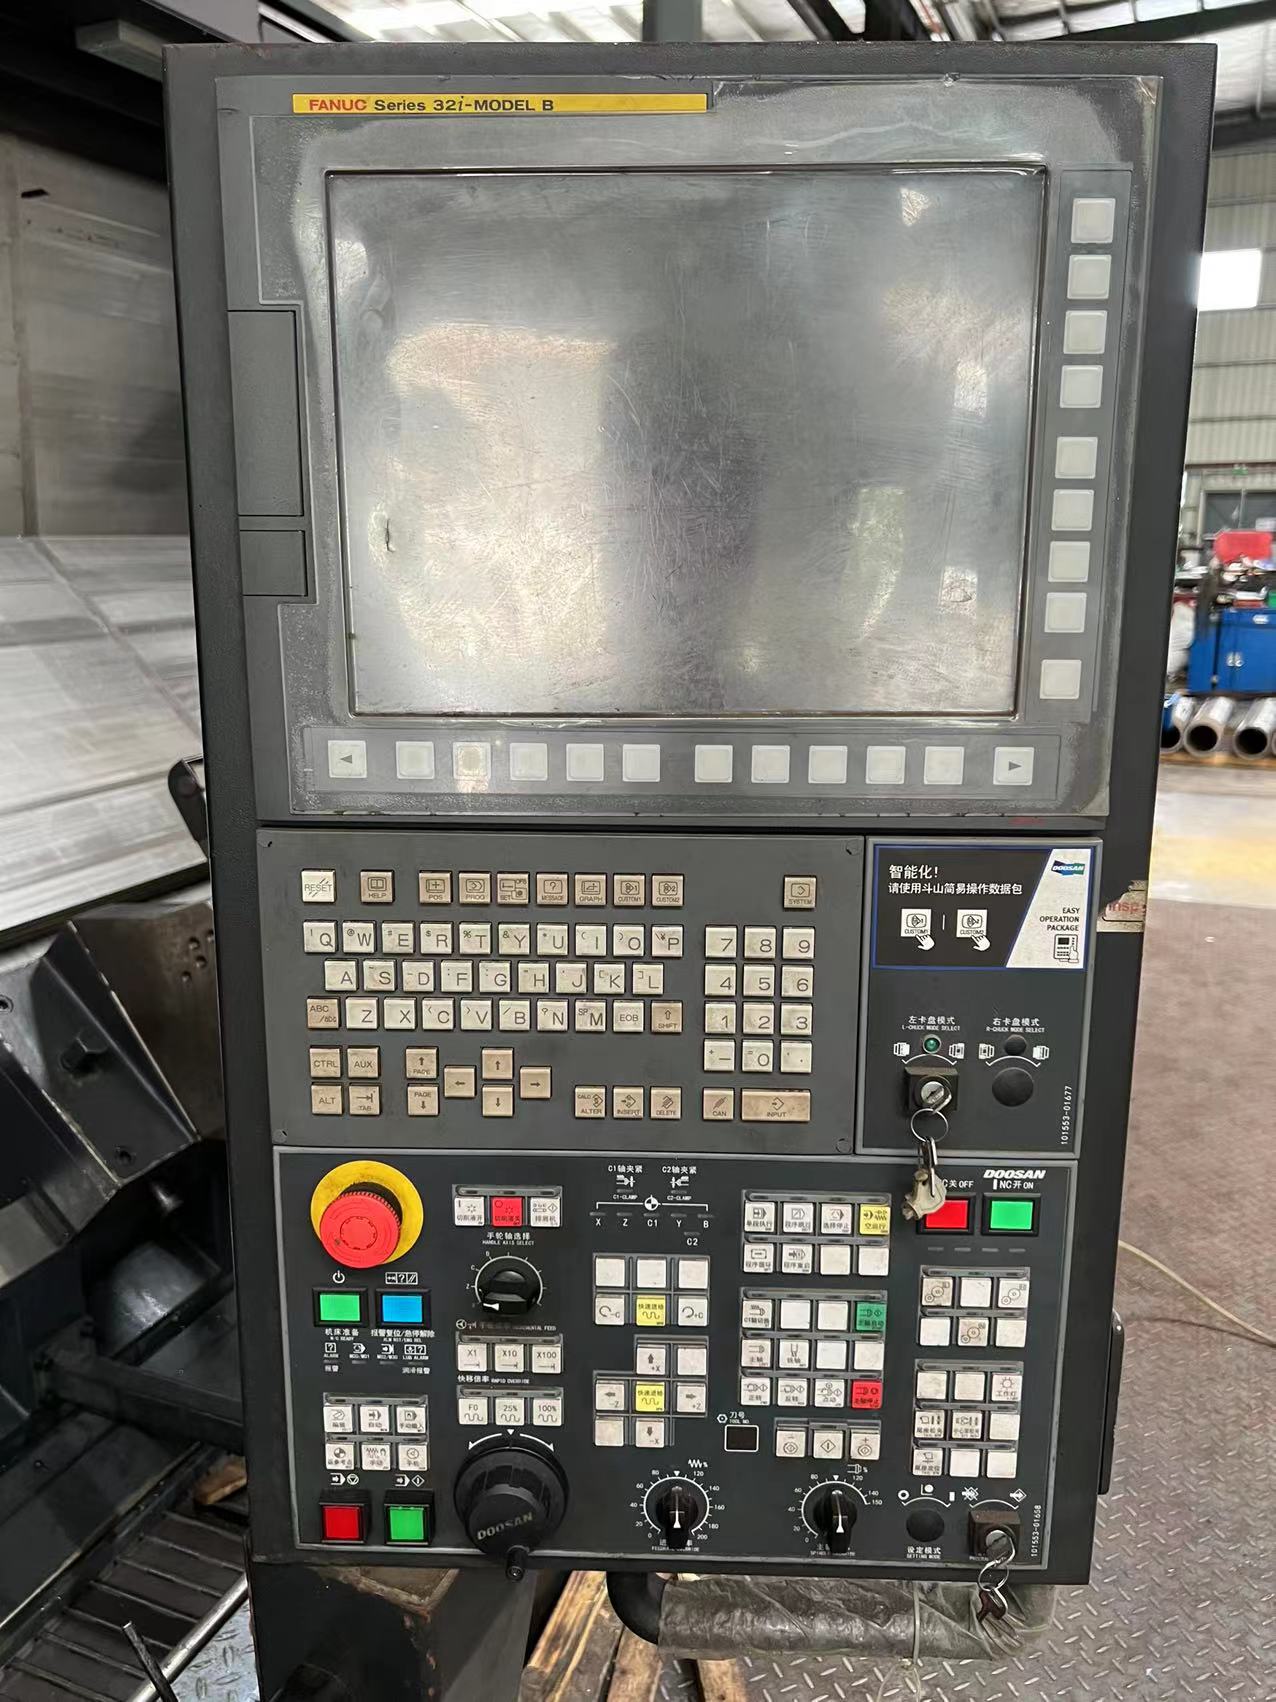
| DBC 130 | Horizontal boring mill | 2,500 rpm | 26–35 kW | Geared spindle, low-speed torque up to 2–3× direct-drive | ≈ 10 m/min | ≈ 13–15 tons | Large box parts, cylinder blocks, heavy castings/weldments — heavy boring & milling |
Note the DBC 130 row carefully: it may be the only Doosan model with a "mere 2,500 rpm" ceiling — yet it is the correct answer for large box parts. Heavy, large-bore work has nothing to do with speed; everything to do with low-speed torque, rigidity, travel, and table load.
Conversion Formulas (the three steps every buyer must run)
① Speed from cutting velocity: $$n \ (rpm) = \frac{Vc \times 1000}{\pi \times D \ (mm)}$$
Machining a φ100 mm 45# steel disk at the recommended Vc ≈ 150–200 m/min → 480–640 rpm. Here a "15,000 rpm max" is meaningless — low-speed torque is the deciding factor.
② Power/torque interchange: $$P \ (kW) = \frac{T \ (N·m) \times n \ (rpm)}{9550}$$
Heavy turning of a φ100 steel part (3 mm depth, 0.4 mm/rev feed, cutting force ≈ 3,500 N): cutting torque ≈ 175 N·m, requiring ≈9.2 kW at 500 rpm. Check against the Lynx 2100 (15 kW motor, spindle torque ceiling ≈ 169 N·m) — torque exceeds its limit by ~4%, with zero headroom; sustained production will throw overload alarms. You must step up to a higher-torque model or reduce depth/feed. This is the key lesson: "9.2 kW is fine" on paper hides the fact that 175 > 169 N·m — check power AND torque together.
③ Large box-part case (why the DBC 130's "low speed" is exactly right): Machining a φ630 mm bore in a reducer casing at recommended Vc ≈ 90–100 m/min: $$n = \frac{100 \times 1000}{\pi \times 630} \approx 50 \ rpm$$
Speed is extremely low, but rough boring demands 1,500–2,000 N·m of torque. A direct-drive spindle may deliver only a few hundred N·m at this speed — only a geared spindle can step down the motor's high-speed torque to "crank" the required torque at 50 rpm. This is the DBC 130's entire reason to exist.
④ Cycle-time check (rapid traverse impact): Time saved per move = move distance ÷ rapid-traverse speed difference. Going from 30 → 48 m/min: a single 1.2 m positioning move drops from 2.4 s to 1.5 s, saving ≈0.9 s per move; a box part with 3 positioning moves per piece saves ≈2.7 s, and at 80,000 pieces/year that's ≈60 hours ≈ 7.5 shifts.
Core Technical Logic: Four Rules That Decide Matching Success
1|Spindle drive types — the real difference: direct-drive vs belt vs gearbox
- Direct-drive spindle: motor rotor integral with the spindle — high speed (12,000–20,000 rpm), low vibration, fast acceleration; ideal for light-cutting, high-speed parts in aluminum, copper, and plastics. Low-speed torque is bounded by the motor.
- Belt drive: lower cost, torque can be stepped up; suits the general 8,000 rpm platform, better mid/low-speed torque than direct-drive but slightly less high-speed rigidity.
- Gearbox spindle: low-speed torque up to 2–3× direct-drive; purpose-built for large-diameter steel, forgings, and interrupted cutting — shops machining stainless/high-hardness steel should prioritize the gearbox version over chasing rpm. The DBC 130's φ130 mm spindle comes standard with a gearbox — a "full-geared heavy-load system" designed specifically for large castings and box parts.
Selection mantra: "soft materials — look at speed; hard materials — look at torque; heavy loads — look at the gearbox (plus rigidity and load capacity)."
2|The torque–speed plateau: the spec that belongs on your purchase order more than "max speed"
Doosan brochure ratings are S1 continuous duty; short heavy cuts can transiently overload ~25%. But if you force a heavy steel roughing cut in the torque curve's collapse zone (high-speed, low-torque region), the motor will overheat and alarm quickly. Correct approach: request the model's torque–speed curve from the sales rep, overlay your peak cutting-torque demand, and confirm the operating point sits below the curve with 20% headroom. For the DBC 130, verify the 50–200 rpm low-speed torque output, not the max speed.
3|Rapid traverse and the process: bigger is not always better
Rapid-traverse gains matter only when positioning time is a large share of cycle time (multi-hole drilling, peck tapping, box-face changes). For deep-hole drilling and large-diameter rough turning where cutting is ~80% of the time, 36 vs 48 m/min is nearly imperceptible. Optimize the cutting parameters first, then talk rapid traverse — get the order wrong and you spend money where no one can see it. The DBC 130's ≈10 m/min looks slow, but with huge workpieces and long cutting times, positioning share is low and the cycle penalty is negligible.
4|Large box parts: why jobs a VMC "can't carry" go to a horizontal boring mill
- Rigidity: HBM table load, short spindle overhang, and floor-type bed let large face mills and big boring bars cut stably — none of the VMC "excessive tool-tip overhang" deflection.
- Multi-face machining in one setup: with a B-axis rotary table, all four/multiple faces of a box complete in one setup, eliminating the accuracy loss and time of repeated VMC setup and probing.
- Travel and load: the DBC 130 reaches ~3,000 mm in X and ~2,000 mm in Y, with a rotary table rated ~13–15 tons — far beyond any VMC. Parts over 5 tons that need large bores or big face milling belong in the HBM selection ledger.
3. Real-World Application Cases (Quantified)
Case 1: Automotive Parts Plant · VMC Torque Upgrade (Medium-Small Workpieces)
Background: An East China automotive parts supplier machining steering-knuckle blanks, roughing + finishing, material 42CrMo forging, φ95 mm spindle bore + 3 side holes, previously on a domestic VMC with frequent roughing "stall" overloads and a monthly scrap rate of 1.8%.
Diagnosis: cutting torque demand ≈ 168 N·m (2.8 mm depth, 0.35 mm/rev feed); the old 8,000 rpm belt spindle delivered only ≈120 N·m at 400 rpm → a ~28% torque gap.
Solution: replaced with a Doosan DNM 5700 with the high-torque spindle option (18.5 kW motor); the HT option's torque at 400 rpm is substantially above the standard ≈118 N·m (the same-family DNM 4500 HT reaches ≈286 N·m — verify the DNM 5700's exact value against the latest brochure), comfortably covering the 168 N·m demand with margin. Roughing depth raised to 3.5 mm, feed to 0.45 mm/rev; 40-tool magazine + 48 m/min rapid to compress tool change and positioning.
Quantified results after 12 months:
| Metric | Before | After | Change |
|---|---|---|---|
| Roughing cycle time per part | 7.2 min | 4.6 min | Cycle time down 36% |
| Peak spindle load | 118% (frequent overload alarms) | 78% | Load down 34% |
| Monthly scrap rate | 1.8% | 0.6% | Scrap down 67% |
| Energy per part | baseline 1.00 | 0.86 | Energy down 14% |
| Tooling cost per part | baseline 1.00 | 0.72 | Tooling down 28% |
Bottom line: cycle time 7.2 → 4.6 min = machine output up ~56% (not merely 36%); the ~35% monthly output lift under the same crew and shifts is the conservative figure constrained by setups, chip handling, and loading/unloading — the roughing bottleneck itself has nearly doubled. Payback on cycle-time math: ~16 months.
Case 2: Heavy-Equipment Plant · Large Box Parts Move to an HBM (DBC 130)
Background: A North China construction-machinery/reducer supplier machining reducer casings and gearbox housings, ~4.5–6 tons each, HT300 cast iron, requiring φ320–φ630 mm bearing bores + large face milling + side hole patterns. Previously handled on a large VMC via multiple setups and long tools forced through.
Diagnosis:
- Obvious vibration when boring large bores; roundness and position unstable, scrap rate 3.2%;
- 4 setups and probing per part, taking 26 hours per part;
- VMC X/Y travel insufficient — some large faces spliced across setups, leaving visible tool marks.
Solution: introduced a Doosan DBC 130 horizontal boring mill (φ130 mm geared spindle, BT50, rotary table rated ~13–15 tons — ample margin over the 4.5–6 ton parts, FANUC 31i, 60-tool magazine + auto chip conveyor), machining rough-bore, large face, and B-axis side-hole patterns in one setup.
Quantified results after 12 months:
| Metric | Before (large VMC) | After (DBC 130) | Change |
|---|---|---|---|
| Total time per part | 26 h | 14.5 h | Cycle time down 44% |
| Setups per part | 4 | 1 | Setups down 75% |
| Scrap rate | 3.2% | 0.8% | Scrap down 75% |
| Large-bore roundness/position | partially out of tolerance | ≤ ±0.02 mm | Stably in tolerance |
| Energy per part | baseline 1.00 | 0.72 | Energy down 28% |
| Occupancy of high-end VMCs | fully occupied | freed for precision mold work | Bottleneck capacity unlocked |
Bottom line: cycle time 26h → 14.5h (−44%) + scrap 3.2% → 0.8% (−75%); at 400 parts/year → ~4,600 VMC hours released per year and scrap losses cut ~75%, payback ≈ 28 months, with table-load headroom reserved for even larger box parts later.
4. FAQ
Q: For machining aluminum, should I choose the 12,000 or 15,000 rpm Doosan VMC spindle?
A:
- Compute it: Vc = π × D × n / 1000. A φ20 mm aluminum part needs n ≥ 6,400 rpm to hit the recommended Vc ≥ 400 m/min — 12,000 rpm is already ample.
- The 15,000 rpm direct-drive advantage is high-speed milling with small tools (φ3–6 mm finishing); upgrade only if small-tool surface finish dominates your process.
- Going to 15,000 rpm usually sacrifices some low-speed torque and adds cost — for medium/large-diameter aluminum parts, the 12,000 rpm version is the best value.
Q: How do I convert torque and power? How do I tell if a Doosan CNC machine is "strong enough"?
A:
- Formula: P(kW) = T(N·m) × n(rpm) / 9550, or inversely T = 9550 × P / n.
- Get the recommended cutting force from your process handbook → compute the cutting-torque demand.
- Plot the operating point on the Doosan model's torque–speed curve and confirm delivered torque ≥ demand × 1.2 (20% headroom).
- In production, take it one step further: split roughing and finishing so peak load stays within 80% of rated.
Q: When should I choose the DBC 130 HBM over a large vertical machining center?
A:
- Workpiece weight: parts over 3–5 tons that must be carried and rotated in full — VMC table load is typically at its limit; go straight to an HBM (DBC 130 rated ~13–15 tons).
- Bore pattern: box/cylinder parts dominated by φ300 mm+ bores, deep pockets, and multi-face work — the HBM's short spindle overhang + B-axis rotary table excel, completing all faces in one setup.
- Accuracy and rigidity: heavy parts needing stable bore roundness and position — "long-tool forcing" on a VMC causes deflection and vibration; the HBM's tool-tip-to-bearing distance is short and rigidity is better.
- What the VMC should keep: medium-small precision molds, complex aluminum surfaces, high-mix low-volume — those are VMC/5-axis strengths. Pulling large box parts off the VMC is step one to unlocking capacity.
Q: How much does rapid traverse actually affect cycle time?
A:
- The impact depends on the positioning-to-cycle-time ratio, not the absolute speed.
- Multi-hole drilling, tapping, and box-face changes: 30→48 m/min saves 5–15 s per part — significant at high volumes.
- Deep-hole drilling and large-diameter rough turning (cutting is ~80% of time): rapid-traverse gains are negligible — invest in cutting power first. On the DBC 130, cutting time dominates, so 10 m/min rapid is imperceptible in cycle time.
- Before buying, run your own math with «average positioning distance ÷ speed difference» — more reliable than a sales pitch.
Q: For stainless/high-hardness steel, should a Doosan be fitted with a gearbox spindle?
A:
- Stainless (304/316 types) has poor thermal conductivity and work-hardens — it needs low-speed, high torque; the gearbox version delivers 2–3× direct-drive torque in the 200–600 rpm range.
- Rule of thumb: roughing diameters ≥ φ80 mm or cutting power > 12 kW → strongly recommend the gearbox version.
- For light finishing with small stock, a direct-drive high-torque model (e.g., DNM 5700) can work, but chip breaking and tool life suffer.
- Verify with a test cut: run your actual workpiece continuously for an hour and watch the spindle-load waveform for stability — that's the hardest evidence.
Q: How much torque difference is there between the Doosan Lynx 2100 and PUMA series?
A:
- Lynx 2100: 15 kW spindle; mid/low-speed torque covers general φ≤120 mm carbon-steel disk/shaft work.
- PUMA 240/2600: significantly stronger spindle power (e.g., PUMA 2600 ≈ 30 kW) with higher low-speed torque output — for large-diameter castings/forgings heavy turning.
- Selection logic: workpiece diameter and material hardness set your torque demand → compare the two torque curves → when demand exceeds ~80% of the Lynx mid/low-speed ceiling, go straight to PUMA instead of relying on overload margin.
- Price, footprint, and energy differ notably — "adequate plus 20% headroom" is the best value boundary.